What is the VIP6025T cutting area?
The published entry is 6000*2500mm, the largest pair of area dimensions in the VIP-T table. It is used for the sheet-area comparison.
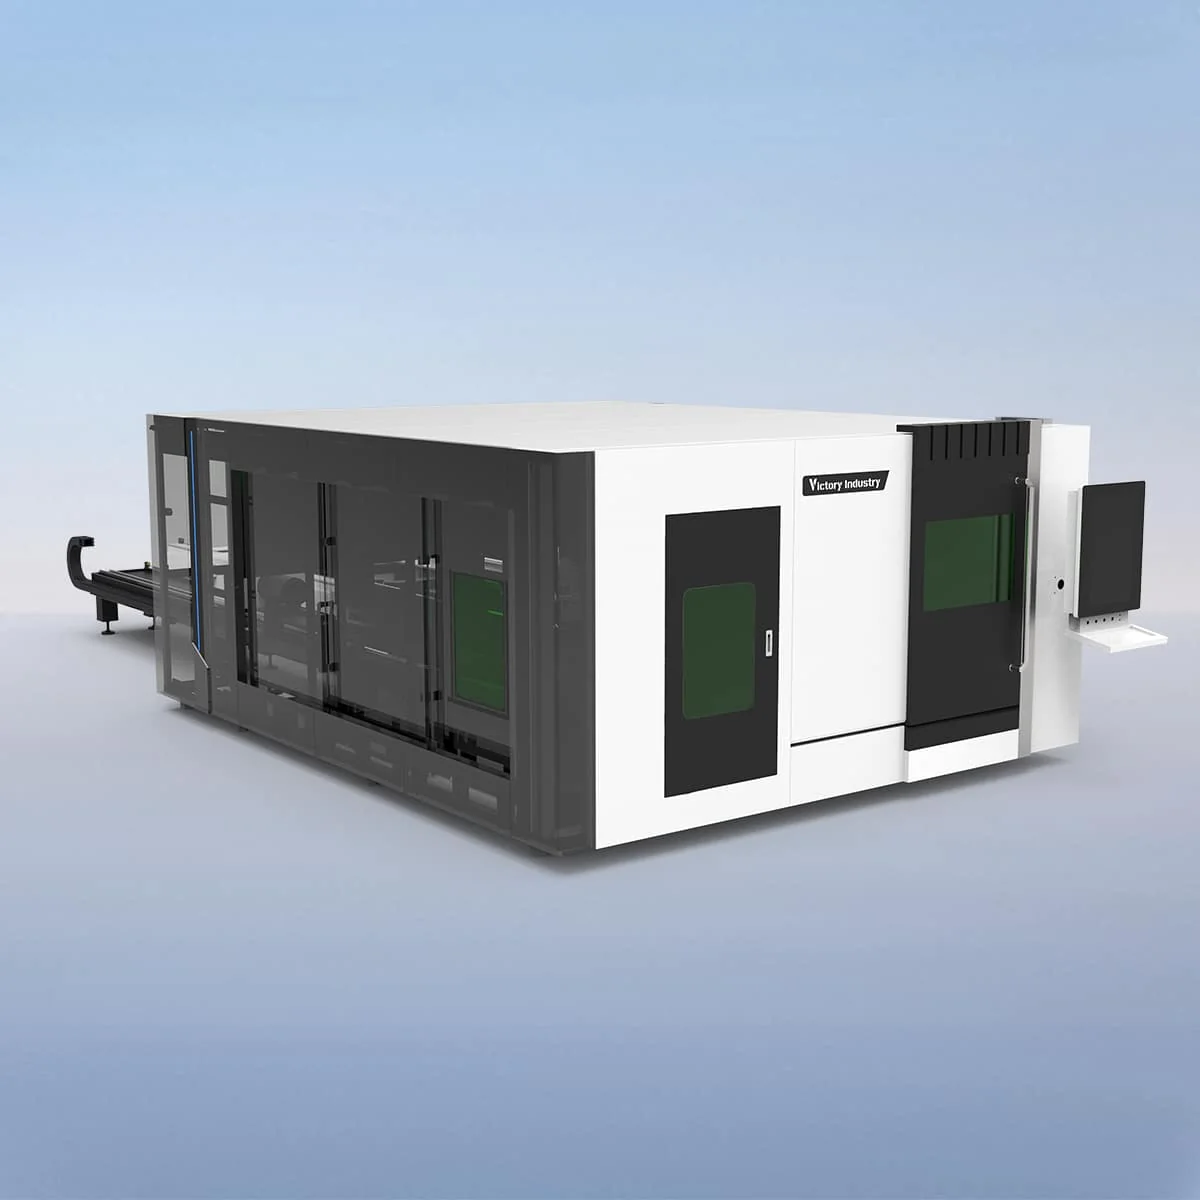
Tube And Sheet Laser Cutting Machine
VIP6025T specifications list a 6000*2500mm cutting area, the largest pair of area dimensions in the VIP-T table. The model belongs to the tube and sheet laser cutting range and has a published power range of 1500-20000W. Maximum linkage speed is listed as 140m/min.
A large-format combined project needs two clear workpiece descriptions. Explain the sheet requirement that led to this area, then describe the tube section and drawing independently. The size and motion entries do not establish tube processing limits or a completed-part output for the planned work.
| Specification | VIP6025T |
|---|---|
| Cutting Area | 6000*2500mm |
| Laser Head | Raytools, WSX, BOCI, Osprey |
| Laser Power | 1500-20000W |
| Laser Generator | Raycus, MAX, IPG |
| Control System | CypCut, Weihong |
| Servo Motor And Driver | Fuji, Delta, Yaskawa |
| Guide Rails | Taiwan Linear Rails |
| Reducer | Japan Shinbo, France Mortori |
| Max. Acceleration | 1.3G |
| Max. Linkage Speed | 140m/min |
| Z Axis Travel | 300mm |
| Positioning Accuracy | 0.05mm |
| Repositioning Accuracy | 0.03mm |
Configuration options vary by model. Confirm the final specification, selected components and operating requirements with your quotation.
The VIP6025T cutting area differs from VIP3015T at 3000*1500mm in both dimensions. Comparing it with VIP6015T at 6000*1500mm retains the 6000mm entry while changing the other dimension. Use the incoming sheet formats to explain which size comparison is relevant.
The table lists maximum acceleration of 1.3G and Z axis travel of 300mm. Its 140m/min maximum linkage speed is not a material cutting speed. Keep the motion labels intact when comparing equipment and provide an actual drawing if the purchase depends on a production-time question.
Positioning Accuracy is 0.05mm and Repositioning Accuracy is 0.03mm. Mark the required component dimensions on the sheet and tube drawings. Those requirements should remain distinct from the general machine specification, without implying a test result or guaranteed outcome for unspecified parts.
For a VIP6025T fiber laser cutting machine brief, identify current sheet jobs separately from possible future large-format work. Give material grade, thickness, stock dimensions, drawing revision and quantity for each representative job. Include regular smaller work if it is part of the proposed workload.
The tube brief needs section shape, outside dimensions, wall thickness, material, incoming length and finished features. Ask for the proposed arrangement to be confirmed against those details. The 6000*2500mm Cutting Area does not supply a maximum tube diameter or loading length.
If the equipment comparison involves several component choices, keep both job lists consistent. A revised tube section or new sheet format should be identified before comparing the responses. A combined category does not mean that every future drawing or stock size has already been reviewed.
Where an output requirement matters, state it as a question linked to a particular job reference. Do not use maximum linkage speed to infer a finished-part rate for either group of workpieces. The published model table gives equipment fields, while the application brief supplies the questions that remain to be answered.
The VIP6025T configuration lists Raytools, WSX, BOCI and Osprey heads and Raycus, MAX and IPG generators. Confirm the power rating and proposed head-source combination. Several alternatives in the table are not a statement that every brand is supplied with one machine.
The control choices are CypCut and Weihong. Fuji, Delta and Yaskawa are listed for the servo motor and driver. Keep the selected components in their own quotation fields, with the model and drawing references, so a revision can be compared without losing the equipment description.
The remaining entries include Taiwan Linear Rails and Japan Shinbo or France Mortori reducers. Request overall equipment and installation information for the destination separately from the cutting area. Use the series page for another area comparison or the contact page to send the defined combined-project brief.
The published entry is 6000*2500mm, the largest pair of area dimensions in the VIP-T table. It is used for the sheet-area comparison.
VIP3015T lists 3000*1500mm, so both sheet-area dimensions differ. Tube requirements still need their own description and confirmation.
The table does not establish that relationship. Supply the tube section, stock length and drawing for a specific response to the proposed arrangement.
It is maximum linkage speed. It should not be reported as material cutting speed or a finished-part production rate for the project.
Use the same sheet and tube requirements, identify the current drawings, and record the selected power, head, source, controls and drives. Keep unresolved application questions visible.
Compare VIP-T Laser Cutting Machine models
Share your material, dimensions and process. Start a conversation about the right configuration.